

Hot Keyword:
Author:YISEN Pouch Packing Machine Manufacturer TIME:2026-08-30
Specify compressed air at the automatic packing machine connection, under the production conditions the factory intends to use. Agree pressure, peak demand, consumption basis and air quality for the delivered configuration, then connect those requirements to the receiving network and its maintenance owners. A compressor rating or a stationary gauge reading cannot establish the complete point-of-use condition.
Begin with the equipment actually included in the quotation. List pouch grippers, cylinders, valves, filler gates, reject devices, vacuum generation, cleaning blow-off and optional modules where they belong to that configuration. Mark an item absent or outside the order instead of assuming that every automatic packer uses the same pneumatic arrangement.
For each included consumer, ask when it operates and which other consumers act with it. A demand that occurs only during pickup can coincide with another station's movement or rejection. The useful load list therefore explains the sequence behind consumption rather than presenting component names without an operating context.
Keep separately supplied downstream handling visible. If it shares the factory network, its demand still matters to the site's utility review even when it is not included in the base-machine price. Identify who supplies its information and who brings the separate loads into the combined assessment.
When an option is added, return to this list before accepting the old utility submission. An unchanged base-machine cycle does not establish unchanged peak demand for the complete line. Record the configuration revision against the load list so purchasing and commissioning refer to the same scope.
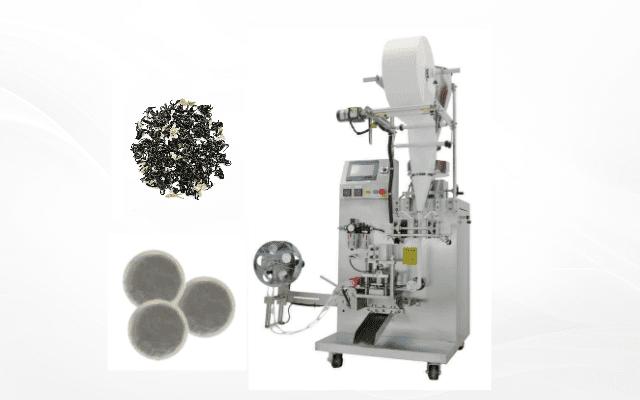
Round-tea equipment shown as one automatic packing application; no pressure, flow or air-quality measurement is shown.
Ask the supplier to state the required operating pressure range and the basis of its flow or consumption figure. Pressure, average consumption and a short simultaneous demand answer different questions. Keep the original units and stated conditions with each entry; a single number headed air requirement leaves the comparison incomplete.
Separate the pressure available before cycling from the lowest value observed while the line performs the agreed work. A satisfactory static regulator reading cannot establish that the supply remains within the requirement when several devices act together. Conversely, an observed pressure fall needs its production event recorded before a cause is assigned.
Give average consumption and peak demand separate places in the utility record. The supplier's explanation should identify the coincident operations behind a proposed peak, including vacuum generation where it belongs to the delivered design. Do not substitute an average figure simply because it is the only value printed in the quotation.
Leave an undefined consumption basis open for clarification. The site designer needs to understand what the supplied figure represents before using it to assess generation, storage and distribution. Purchasing should obtain that explanation rather than create a margin that conceals the missing information.
Specify the air condition at the machine inlet as part of the purchase interface. Ask the equipment supplier for its dryness, filtration, oil, particle and condensate requirements, including restrictions on lubricated air. Align those requirements with the site's qualified utility design and the product environment.
Do not infer a universal oil-free requirement from the words automatic packing machine. Equally, do not assume that air acceptable elsewhere in the factory meets the delivered components' requirements. The written submission should say which condition applies at this connection and how that condition will be checked.
Connect each quality requirement to the equipment and maintenance that preserve it. Record the dryer, filters, drains and relevant pipe condition, with service ownership and the supplier's inspection or replacement guidance. A list of installed treatment devices is incomplete if nobody is responsible for their condition after handover.
Keep oil, water, rust and pipe debris away from the product and packaging areas through the site's approved procedures. Maintenance or blowdown should not send contamination toward the machine. This is a requirement to review with the responsible teams, not permission to improvise a cleaning method.
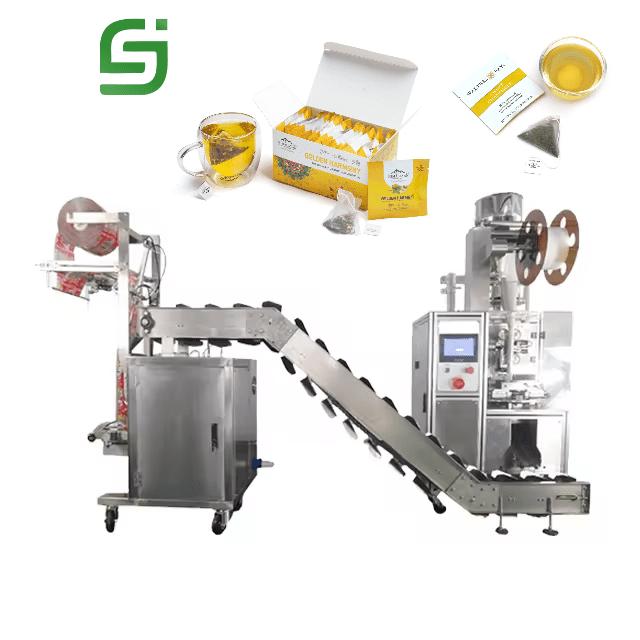
This product illustration shows two units and their transfer layout. It does not establish the utilities or supplied options of an ordered line.
Review the compressor, receiver, dryer, filters and distribution network as one utility path. Include the proposed connection, pipe run, distance, elevation, fittings and shared equipment in the designer's assessment. Selecting a compressor from a machine average alone leaves the intervening supply path unexplained.
Ask the site utility designer to keep measured production load separate from estimated leakage, future additions and other planning allowances. A practical reserve needs a stated basis. An unexplained percentage or a larger compressor does not resolve an undersized restriction, an unsuitable receiver arrangement or a network assumption that has not been checked.
Where several machines share a branch, identify the busy combination the factory expects to operate. Review that combination rather than treating each machine's isolated requirement as evidence about their simultaneous condition. Record any equipment not available during the demonstration as a remaining assessment item.
The final utility decision belongs to qualified personnel using the actual proposed network. The machine supplier explains its delivered requirement; the buyer identifies the receiving system and connected loads. Assign the party responsible for reconciling those submissions before commissioning is described as complete.
Measure pressure and relevant flow conditions at the machine connection while the agreed production sequence runs. Retain the upstream condition needed to explain distribution losses. A compressor display alone cannot describe a distant inlet after the air has passed through piping, filters, regulators and local connections.
Tie each observation to a named event. Record whether the line was stationary, running normally, rejecting a pack or recovering after a pause, and identify the shared loads operating at the same time. The lowest inlet observation is useful only when the team can relate it to the condition that produced it.
Compare inlet and upstream information before deciding where a restriction may lie. Preserve the evidence when a local filter, pipe run or another supply element is investigated. Repeatedly increasing a regulator setting can obscure the original condition and should not replace the supplier's and site's approved diagnostic procedure.
Keep instrument identity, measurement location, configuration and operating conditions with the results. If the agreed production load was not represented, state that limit. A measurement from an easier condition remains useful for that condition but cannot silently approve a busier complete line.
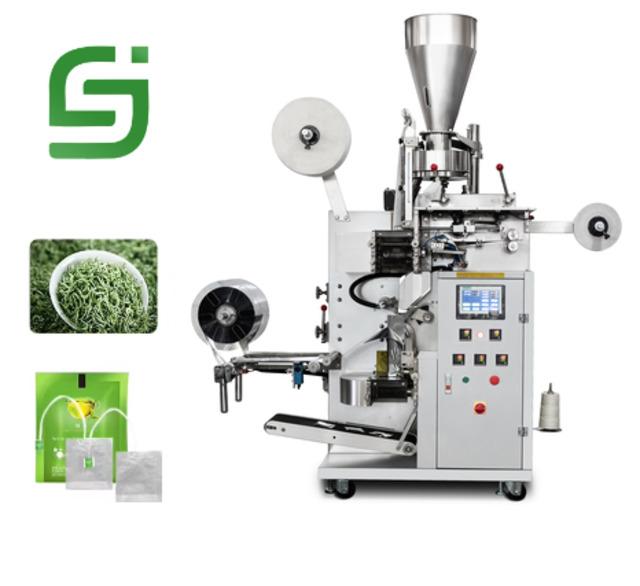
Another tea-packing arrangement, used here for equipment context. Component requirements still come from the delivered configuration, not from this photograph.
Agree a sequence covering startup, ordinary indexing, refill, reject activation, a short stop and restart where those events apply. Include the busiest simultaneous pneumatic event identified in the load review. Have the supplier and site personnel define safe demonstrations and the observations needed for each.
Record pressure and relevant flow observations beside alarms, incomplete motion, pouch faults or filler delays. Keep an observed machine symptom distinct from a confirmed utility cause. This lets the responsible teams investigate the same event without treating every missed pouch action as proof that more pressure is required.
Follow the output after supply returns from an interruption. Confirm the approved alarm or safe-state response, restoration and first acceptable pouches under the agreed procedures. A cleared message alone does not show that the line has returned to its accepted utility and package condition.
The decision table below distinguishes an available record from the evidence still needed. Use it to return a specific unanswered question to the responsible party. It supplies no pressure target, equipment size or universal acceptance limit.
| Record supplied | Decision it supports | Question still open |
|---|---|---|
| Static pressure only | Condition before cycling | Lowest inlet condition during peak demand |
| Average consumption | The declared operating average | Coincident consumers and short demand |
| Compressor-side reading | The recorded upstream condition | Distribution loss and machine inlet result |
| Treatment equipment list | Proposed quality-control equipment | Delivered air condition and maintenance responsibility |
| Complete point-of-use trial | The demonstrated configuration and events | Untested shared loads or later additions |
Give operators and maintenance staff distinct duties for leaks, filters, drains, regulators, hoses and isolation. Follow the equipment and site procedures for shutting off and releasing pressure. Record which conditions require escalation and what verification is needed before released packing resumes after pneumatic work.
Keep the accepted regulator setting and utility limits with the machine record. Discourage undocumented increases used to mask leakage, worn devices or distribution limits. If the required setting appears to change, compare the new observation with the accepted configuration and production event before changing the baseline.
Connect filter and drain care to evidence about their condition rather than a check mark alone. Retain the observations, action, replacement identity where relevant and the verification after work. A recurring issue should return to the responsible maintenance or utility owner instead of being hidden through repeated adjustments.
Train the team to preserve useful fault information. The inlet condition, upstream observation, active machine functions and recent work help distinguish a machine-side issue from a compressor-side or shared-network issue. Clear ownership makes the same evidence usable by both teams.
Close the interface with one agreed utility record. Identify the connection, machine revision, production condition, pressure and flow basis, quality requirements, instruments and responsible parties. Keep accepted limits separate from estimates and attach the open actions with the evidence required to close them.
Use the configured doypack packing machine reference to identify the quoted scope, then reconcile that scope with the actual pneumatic load list. The product reference does not replace the delivered machine's written utility requirement or a site measurement.
State when the baseline must be reviewed: an added module, changed line arrangement, altered compressor network or additional shared factory load can change the comparison. Retain the earlier record rather than overwriting it, so the responsible teams can see which condition was accepted and what the later change affects.
Handover is complete only to the extent demonstrated. Keep an unmeasured capacity or quality condition open, assign its owner and define the required follow-up. The useful purchase outcome is a reproducible point-of-use agreement, not a general statement that the factory has compressed air.
Can a normal static reading close a fault seen only during production?
No. Keep the production event, inlet observation and relevant upstream condition together. The static result does not describe the short demand that accompanied the fault.
What if a quoted consumption figure has no stated basis?
Return that omission to the supplier. Preserve the number as incomplete information rather than inventing conditions for the site design.
Does a treatment equipment list prove the inlet air quality?
It identifies proposed controls. The agreed condition and its verification, along with filter and drain responsibilities, still need to be established.
Who resolves a shared-network question?
The buyer identifies the receiving network and other loads; the machine supplier provides its requirement. Assign a qualified utility owner to reconcile the complete arrangement.
When should the accepted air record be reviewed?
Review changes to the line, options, compressor network or shared load against the original condition. Repeat affected evidence through the responsible teams rather than silently extending approval.
Approve the air interface by connecting the delivered load list, supplier requirements, site network and observed inlet condition. Preserve the operating events and quality controls with their owners, then use that record when a fault or configuration change arises. Leave unmeasured conditions open until the responsible parties provide the missing evidence.
YISEN MACHINERY - The ONE-STOP VFFS PACKING MACHINE SOLUTION SUPPLIER
 Tel: +8617350750975
 Email: info@vffspackingmachinery.com
 MP/WhatsApp: +8617350750975
 Manufacturer Address:Meixi Road, Tongan District, Xiamen,Fujian,China