

Freeze the package boundary for line interfaces
Create a package drawing with three possible layers: infusion filter bag, individual barrier envelope and multi-bag retail pouch. Mark which layer receives the tag, code, tear notch and final seal so the machine boundary is unambiguous.
Record the material code for line interfaces.
Add its dimensions and seal zone to the signed drawing.
Test each substitution against a line can meet net weight at the inner.
Material behaviour sets the limit for package layers
Tea grade and target dose determine the metering method, but they do not identify the package. Dusty fine tea, leafy herbs and blended inclusions need separate flow and cleaning observations before a common feeder is approved.
For Tea grade and target dose determine the metering method, record sample origin, storage and expected variation.
Release its operating window only when the trial can define whether pouch means the filter bag, its outer envelope or a retail pouch before speed, weight control and line integration are compared.

What this application reference can establish
Evidence level B — application reference. The original page asks for high speed, precise weight, automatic tagging, varying pouch sizes and integration in Ecuador. It never resolves the package hierarchy or publishes the installed interface and accepted run data.
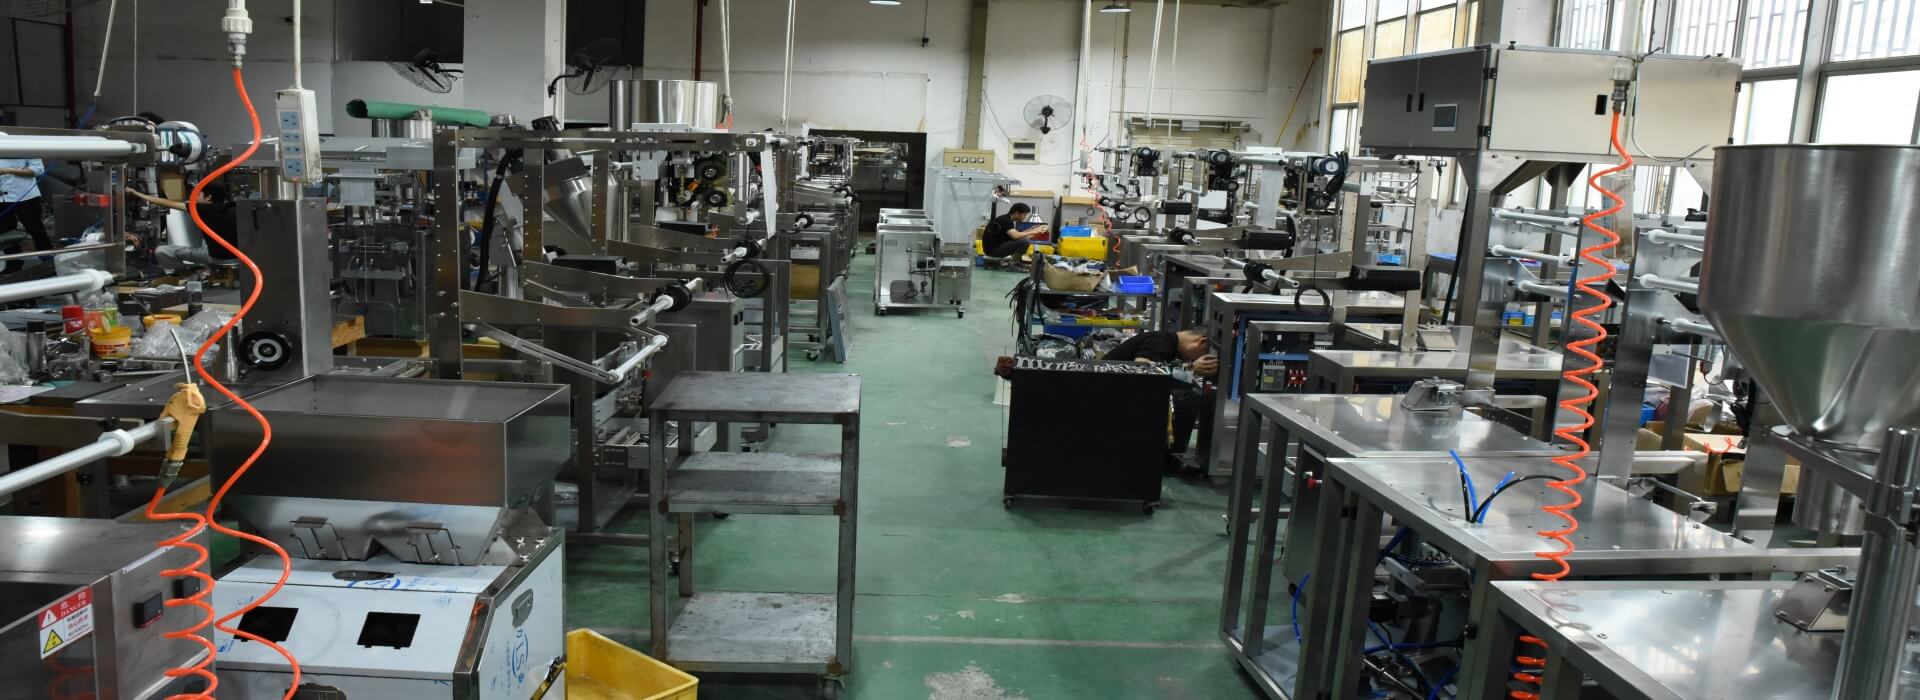
The title and retained images orient the Ecuador tea-pouch definition review toward package layers, line interfaces and pouch-count control.
For the Ecuador tea-pouch definition review, archived transaction and outcome language remains outside acceptance for package layers.
Release matrix for package layers, line interfaces and pouch-count control
| Decision area | Case-specific observation | Required action |
|---|---|---|
| Evidence | The original page asks for high speed, precise weight, automatic tagging, varying pouch sizes and integration in Ecuador. | Keep customer and outcome claims outside approval. |
| Product | Tea grade and target dose determine the metering method, but they do not identify the package. | Use production-representative samples and record variation. |
| Package | Create a package drawing with three possible layers: infusion filter bag, individual barrier envelope and multi-bag retail pouch. | Freeze drawing, material code and retained sample. |
| Main risk | A line can meet net weight at the inner bag and still fail because the envelope jams or the retail pouch count is wrong. | Turn the risk into a visible reject and test criterion. |
| Release gate | Define whether pouch means the filter bag, its outer envelope or a retail pouch before speed, weight control and line integration are compared. | Sign the evidence record before commercial release. |
Treat the machine as one sequence for line interfaces
The proposed flow may include tea dosing and filter forming, transfer to an envelope, counting and insertion into a retail pouch. Integration should name every handoff, sensor and responsibility rather than use one broad pouch-machine description.
A line can meet net weight at the inner bag and still fail because the envelope jams or the retail pouch count is wrong. Keep inner-seal, tag, transfer, count and final-pouch defects as different acceptance categories.

Assign owners for installation conditions in Ecuador
For Ecuador, verify existing conveyor height, signal exchange, electrical supply, compressed air, floor space and ambient humidity. Label approval and food-contact status depend on the selected package layers and remain buyer-controlled checks.
Assign a named owner in Ecuador to every measured input for package layers, line interfaces and pouch-count control.
At the Ecuador site, use actual room conditions, utilities and local review for package layers.
Build the sample run around a line can meet net weight at the inner
Approve one complete package path with production materials. Record inner-bag dose, tag position, envelope leakage if used, pouch count, code location, jam recovery and the effect of changing to the largest requested pouch.
For package layers, line interfaces and pouch-count control, keep samples, consumable lots, settings and rejects in time order.
Evidence must cover a line can meet net weight at the inner after an interruption and restart.

Handover must preserve package layers, line interfaces and pouch-count control
The interface document should assign ownership for upstream tea supply, each package stage and downstream case packing. Training must include recovery without losing count or mixing unverified inner bags into accepted retail pouches.
Version the setup that releases package layers, line interfaces and pouch-count control.
A future SKU outside pouch-count control receives its own sample record and re-test.
Evidence questions for the factory trial
Which line interfaces input is frozen before tooling?
The release scope is to define whether pouch means the filter bag, its outer envelope or a retail pouch before speed, weight control and line integration are compared. Any change affecting line interfaces requires a recorded re-test.
What preserves pouch-count control after handover?
Keep package layers, line interfaces and pouch-count control beside retained packs, reject examples, training records, critical spares and open actions.
What must the trial prove about a line can meet net weight at the inner?
Run production samples around a line can meet net weight at the inner. Keep interventions and open actions beside evidence for package layers, line interfaces and pouch-count control.
Can the Ecuador tea-pouch definition review be treated as a completed project?
No cited order or signed acceptance appears in the Ecuador tea-pouch definition review archive. Decide package layers from current samples.
Conclusion
Move this application forward only when package layers, line interfaces and pouch-count control agrees with measured site inputs and retained samples.
Use the related Tea Bag Pouch Packing Machine range as a configuration reference for package layers. Build current acceptance around line interfaces and a line can meet net weight at the inner; keep the archived outcome outside approval.

 Tel: +8617350750975
 Email: info@vffspackingmachinery.com
 MP/WhatsApp: +8617350750975
 Manufacturer Address:Meixi Road, Tongan District, Xiamen,Fujian,China